
Do not hold or reject a tape roll lot based on one curl or tube symptom; first record the shape and direction, repeat the observation under documented conditions at stable line settings, and compare identified rolls. For a converter facing tape curl during converting, the practical decision is not simply whether a strip looks flat. It is whether the observed curl will interrupt dispensing, tracking, lamination or downstream handling—and whether the cause follows the incoming roll or the line conditions. A supplier claim and a process adjustment require different evidence. Changing several settings at once may hide a material problem; rejecting a lot from one uncontrolled run may discard usable stock.
Classify the symptom before changing settings
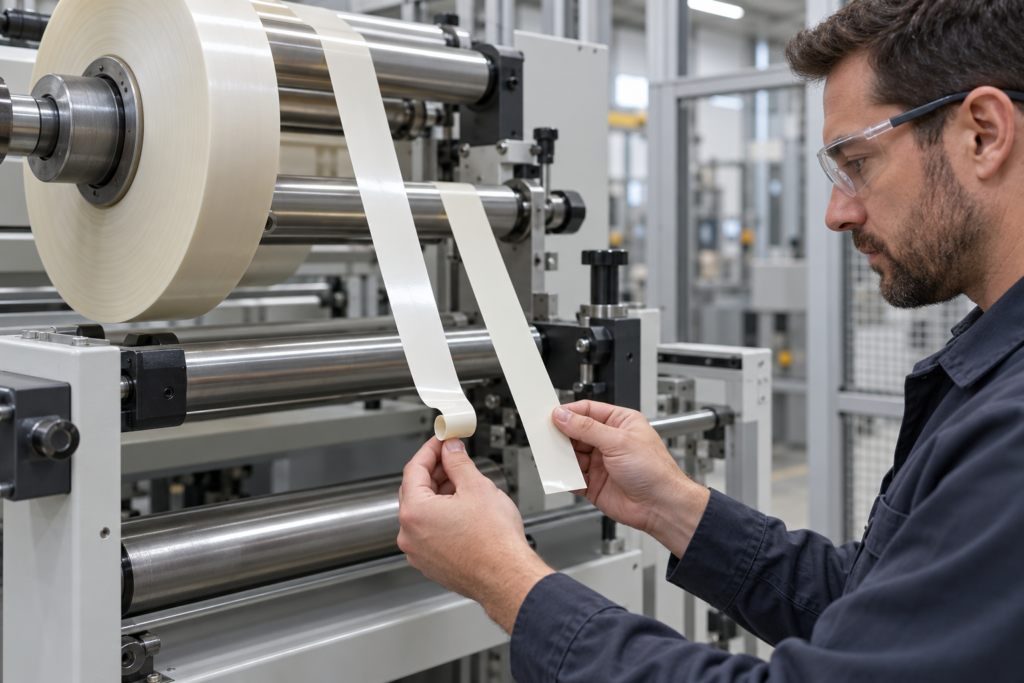
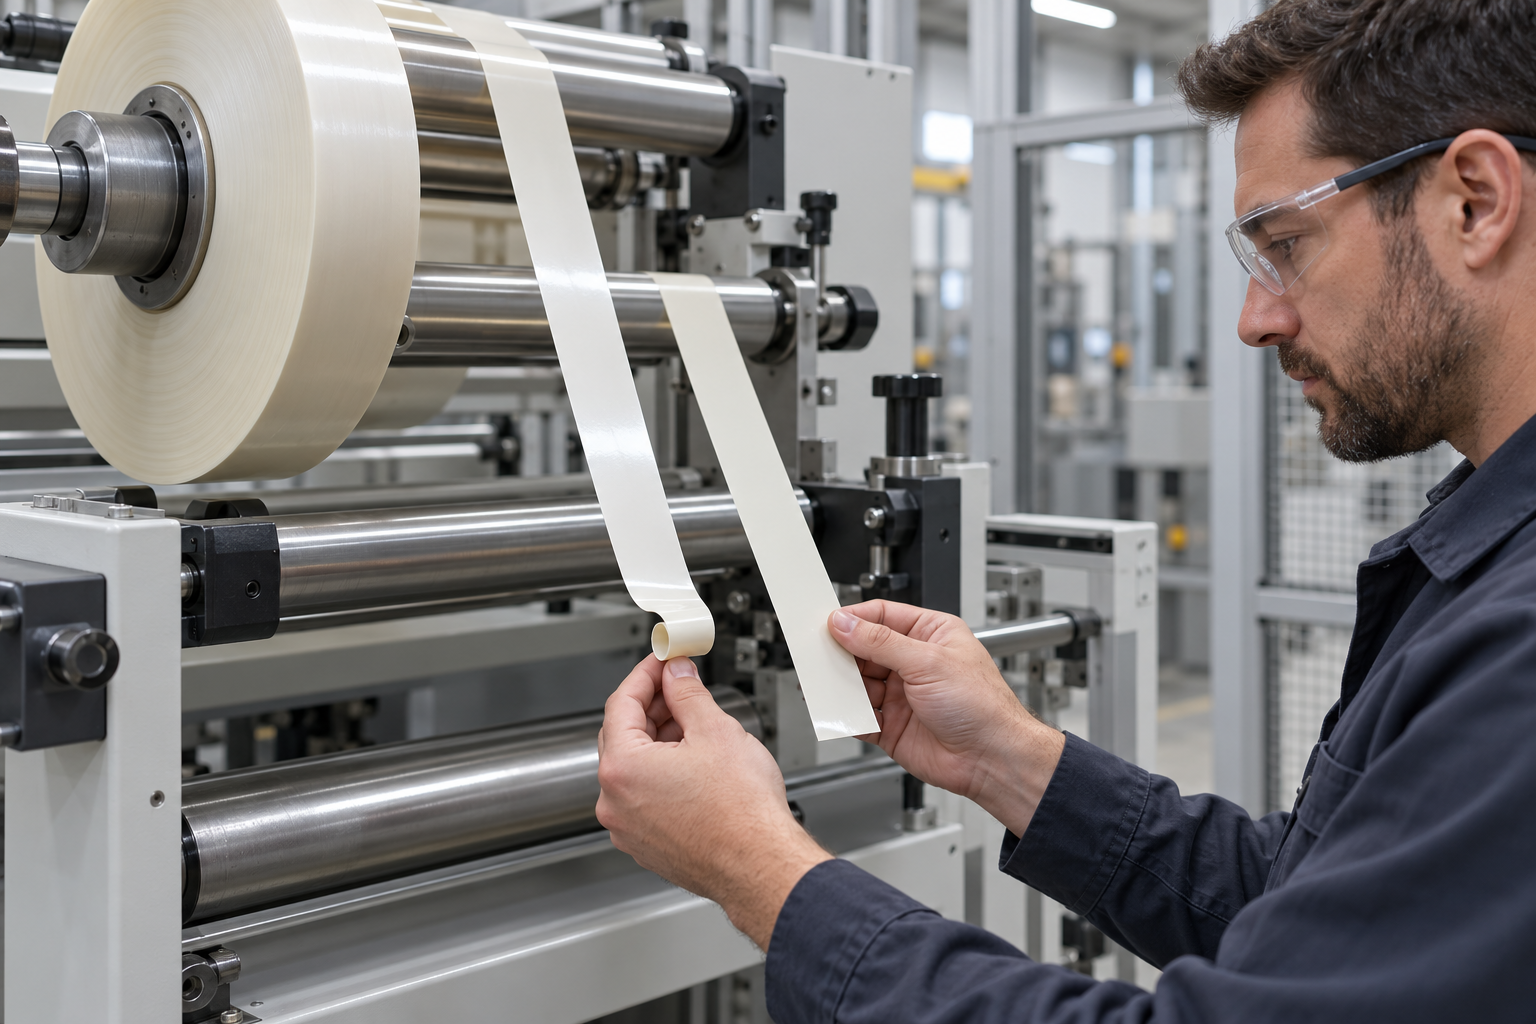
Record what the strip does before it reaches the first process roller. Does it bend along the machine direction, across the web, or does it roll toward itself until the edges approach one another? Note where the behavior begins: at the roll edge, across the full width, after a splice, after passing a roller, or only after lamination. Photograph the strip against a simple reference plane and mark the machine direction and the side that faces the operator.
This description matters because “curl” can refer to more than one shape. Mactac’s industrial tape troubleshooting guide distinguishes tension-related down-web curl from moisture-related cross-web curl or tube formation for certain flexible materials. It also discusses material construction and process history as possible contributors. Those examples help form a diagnostic hypothesis; they do not establish a universal cause for every tape backing, foam carrier, liner or adhesive system.
Keep the terms precise in the production record. A strip that curls along its length is not automatically the same defect as a strip that cups across its width. A tube-like roll-up is another observation. If a web is flat at the unwind but curls after a laminating nip, record that transition rather than describing the entire roll as curled. The point is to locate when and where the geometry changes.
Separate line effects from roll or lot effects
Start with a controlled baseline. Record the tape grade or sample identity, roll and lot numbers, roll width and diameter, core, liner, material orientation, storage history, and the date the roll was opened. Record the machine setup that can influence web handling: unwind tension setting or control mode, speed profile, acceleration, web path, roller condition, nip arrangement, and any changeover or splice.
Then change one variable at a time. If safe for the equipment and product, compare a lower and higher tension condition within the line’s approved operating range. Keep the material, web path and speed profile otherwise stable. Next, compare speed or acceleration while restoring the baseline tension. Do not copy numeric settings from another supplier’s application guide: they are product- and equipment-specific. For example, 3M’s application guidance for its named acrylic foam systems identifies tension, speed, acceleration and roller conditions as factors that can affect stretch in that application. Use that as a reminder to control variables, not as a setting specification for a different construction.
If the symptom changes promptly when a process variable changes, document that relationship and review the line setup before calling the incoming roll defective. The material and process can interact, so this does not prove the roll is fault-free. It does tell the team what to reproduce next. Conversely, if the same roll shows the same curl under repeatable settings, compare another identified roll from the same lot and, when available, a known-good control roll using the same equipment and conditions.
Do not compare samples that have different conditioning histories as though they were equivalent. Storage temperature, humidity, packaging condition and time between opening and processing can matter for some flexible materials. Mactac’s troubleshooting guide notes moisture-related behavior in certain liner and flexible-material cases. Record what is known; if environmental history is missing, mark it as unknown rather than attributing the defect to humidity after the fact.
Build a useful supplier-claim record
A useful escalation package lets the supplier reproduce the observation. Include a short defect description, photos or video showing the direction of curl, roll and lot identifiers, the material orientation, the time or web position where it appears, and the line settings. Preserve an affected sample and an unaffected comparison sample if possible. Note whether the problem occurs before or after the nip and whether the strip returns to a flatter shape after being cut free and allowed to rest.
Agree how samples will be compared before drawing a pass/fail conclusion. Define the conditioning period, unwind or dispensing setup, measurement location, number of rolls or samples, and the production handling outcome that matters to the buyer. The acceptance limit must come from the buyer’s specification or a documented agreement for the actual construction and use. This guide does not set a universal curl value or claim that one visual inspection method qualifies every tape.
When the symptom follows one roll but not another, retain both labels and sample lengths. When it appears across several rolls only on one line, compare the line with a separate approved handling setup before rejecting the material. When it appears across multiple lots under stable conditions, record that pattern and ask the supplier to review construction, winding, liner and storage records. Keep the final disposition tied to the evidence and the actual production requirement.
Connect the diagnosis to the tape construction
A roll is a complete construction, not just an adhesive. Backing or carrier, adhesive layers, release liner, roll width, winding and converting format can affect how the material is handled. LubandArt’s acrylic foam tape product page lists configurable thickness, width, roll length, adhesive system and release liner, with jumbo, converted and finished formats. It also states that final values and suitability are confirmed against the project specification and sample test. The page is a product route; it does not publish a grade-specific curl limit or a guarantee that a roll will run without curl on a particular line.
If the defect appears at a liner interface, distinguish liner release or separation from curl of the backing itself. The PET film versus paper liner guide discusses liner choice for converting; it is useful background, but it does not diagnose this roll’s defect. If the concern is bond failure after lamination, keep that separate from a web-handling problem and use the surface preparation and bond strength guide as a separate diagnostic path.
For an RFQ or sample request, send the tape identity, roll format, liner, width, line speed profile, tension-control mode, roller path, storage history and a photo of the defect. State whether the decision is to improve tracking, reduce curl before lamination, or prevent downstream handling interruptions. A supplier can then review a candidate construction and sample plan against the actual process instead of responding to “tape curls” without context.
Decide when to hold the roll
A temporary hold is reasonable when the defect is repeatable, traceable to identified material, and likely to disrupt the buyer’s documented process requirement. Keep the hold limited to identifiable rolls or lots while evidence is collected. If a controlled comparison shows that the symptom follows only a process setting, correct and document that setting and re-run the approved check. If it follows identified rolls under stable conditions, submit the samples and records for supplier review and agree on disposition.
The practical rule is to make the comparison reproducible before making the disposition irreversible. Classify the shape, document the line and conditioning history, compare at stable settings, and set acceptance criteria for the actual tape and process. That sequence helps a converter distinguish a handling adjustment from a material-quality issue without inventing a universal pass/fail limit.
Frequently Asked Questions
Does curl during unwind automatically mean the roll lot is defective?
No. A single observation does not separate material, storage and line-condition effects. Reproduce the symptom under documented conditions and compare identified rolls before deciding disposition.
What is the difference between down-web curl and cross-web curl?
Down-web curl bends along the machine direction; cross-web curl bends across the width. Mactac describes different potential contributors for certain flexible materials, but the actual tape construction and process must be checked.
Can LubandArt acrylic foam tape be guaranteed not to curl?
The product page does not publish a grade-specific curl limit or guarantee. Share the proposed width, roll length, liner, application equipment and observed defect so the candidate can be assessed and sampled.
Send the tape grade or sample, roll width and length, liner, lot IDs, line speed and tension settings, web path, storage/conditioning history and photos of the curl direction to request a candidate review and controlled sample plan.
Request a quote · [email protected] · WhatsApp +86 180 6469 2463
Need this construction for a production run?
Get a quote