
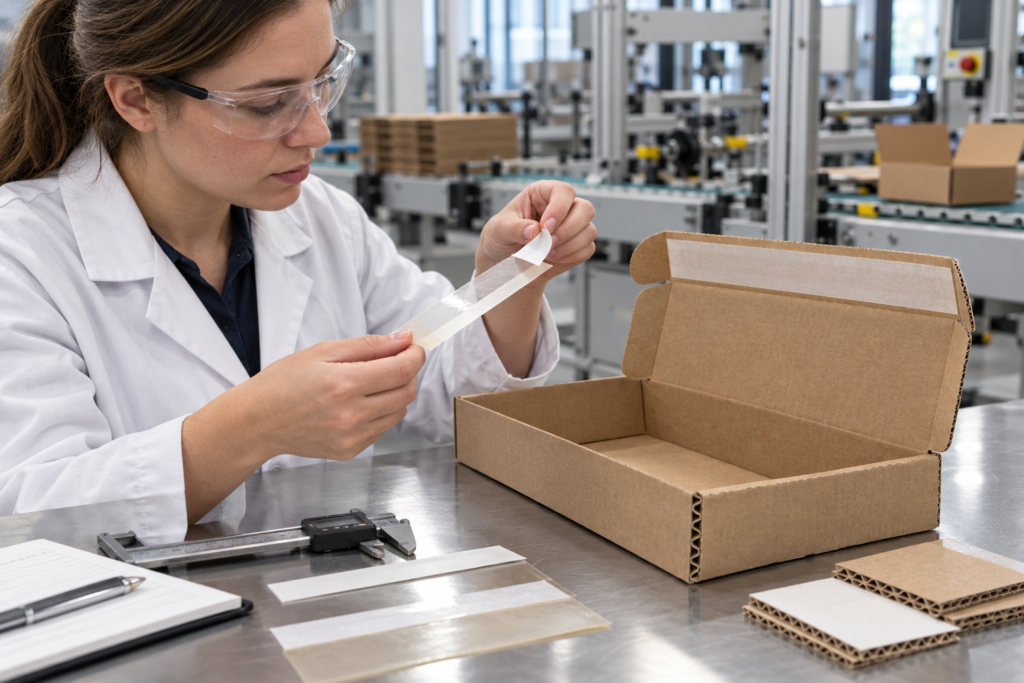
When should double-sided OPP tape be trialed for corrugated carton flap closure, and what must pass?
Approve it only after a production-representative carton and line trial meets buyer-defined closure, process, conditioning and distribution criteria.
Preliminary selection guidance only. No grade-specific LubandArt closure, recycled-board, automation, shipment-load or transit-test evidence was reviewed. Request the current technical data sheet and representative test report for the proposed grade and carton before approval.
When a packaging line needs to close corrugated cartons, double-sided OPP tape is a candidate only if the carton design and the actual application process can hold the flaps to the buyer’s requirements. A film backing does not establish closure strength, and a tape described for “carton sealing” is not automatically qualified for a specific board, line speed, storage condition, or distribution load. Select the architecture first, then test the exact construction on representative cartons.
For double-sided OPP tape carton closure, use the tape only as a trial candidate when the design provides controlled overlap and repeatable contact. Approve it only after the production-representative carton and line meet the buyer-defined closure, process, conditioning, and distribution criteria.
This distinction matters because familiar carton sealing usually refers to a single-sided pressure-sensitive tape applied across the outside of the seam. A double-sided OPP construction has adhesive on both sides of a film carrier and may be used between overlapping surfaces. The geometry, liner handling, application equipment, and failure modes are therefore different. The term double-sided OPP film tape describes a polypropylene carrier family and adhesive on both sides; it does not by itself specify adhesive chemistry, coat weight, backing treatment, liner, or finished performance. Corrugated carton flap closure depends on both the material construction and the package geometry.
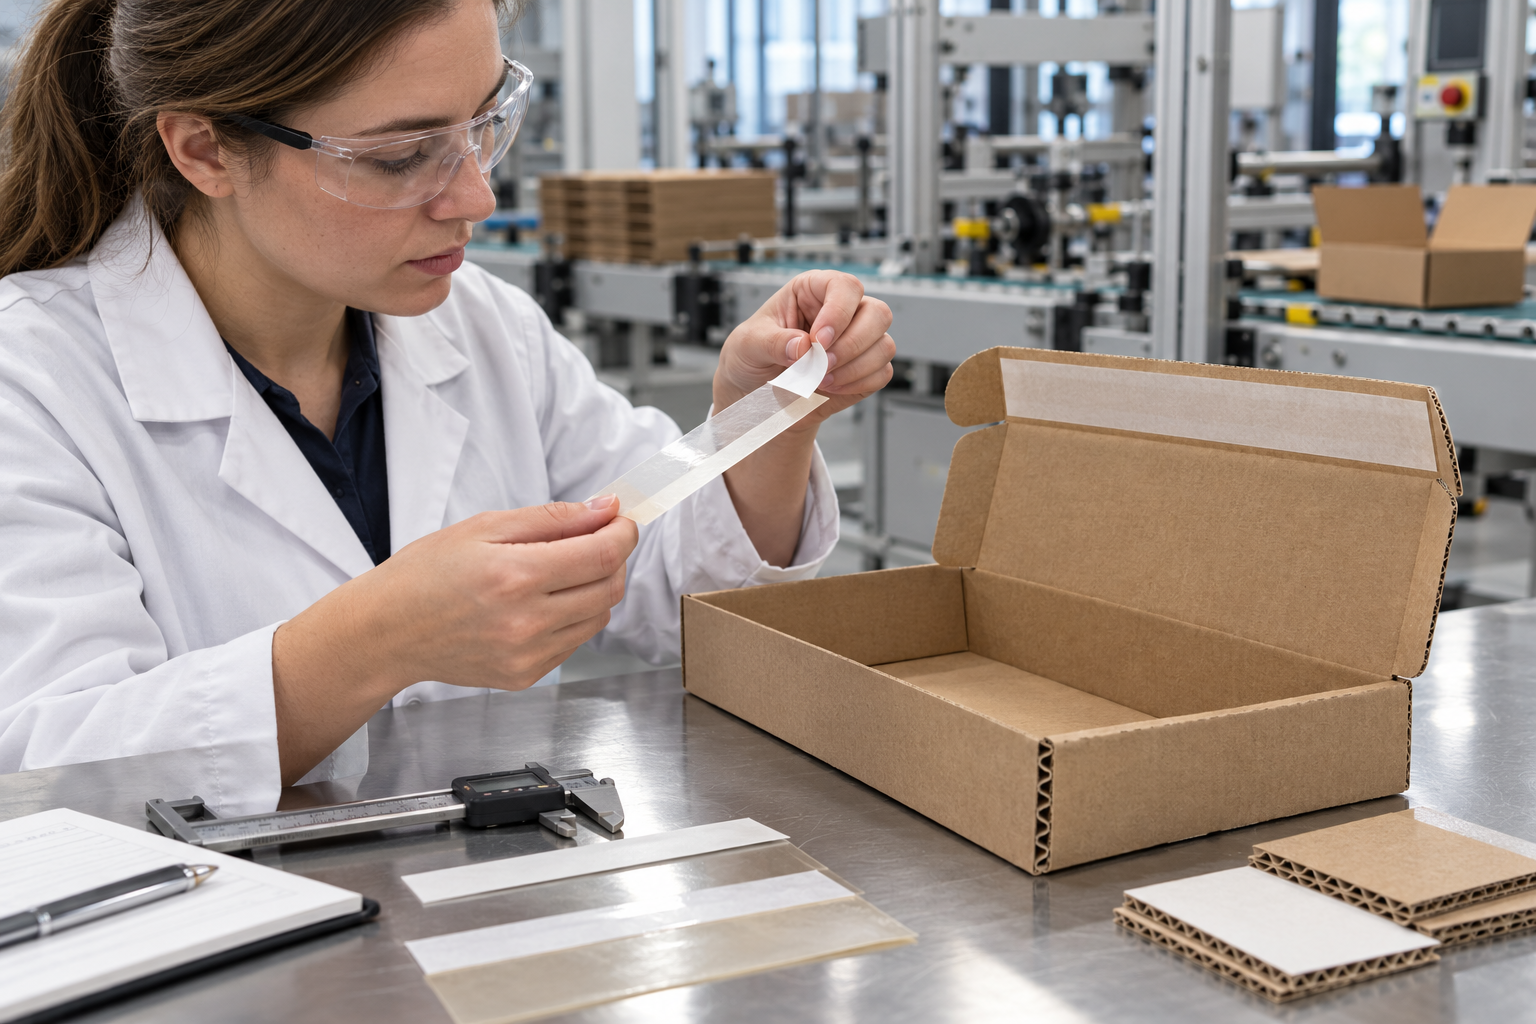
Choose the closure architecture before the tape grade
Start with how the carton is meant to close. A machine-applied single-sided carton-sealing tape bridges the outside of the top or bottom seam. A double-sided tape placed between flaps depends on overlap, contact area, placement accuracy, and how the second surface is brought into contact. Other designs may use hot melt, water-activated tape, staples, interlocking flaps, or a carton specifically engineered for friction or locking closure. These options solve related packaging tasks but are not interchangeable by name alone.
The 3M box sealing tape overview groups carton-sealing products by construction and application. It is a useful reminder that packaging tapes have distinct formats and uses; it does not establish that a 3M tape, or any other supplier’s product, is suitable for this carton. A double-sided film tape should be compared with the buyer’s actual closure options on line performance, carton design, openability, and total process requirements—not just on whether the adhesive feels aggressive on a bench.
If the carton must withstand a defined stacking, handling, or parcel-distribution condition, write that requirement before choosing a closure method. Ask which component is expected to carry the load: the corrugated board, the flap geometry, the adhesive joint, a reinforcing tape, or a combination. Tape adhesion cannot compensate for an undersized carton, weak board, poor seam design, or an unsuitable package for the distribution environment.
Match the construction to the corrugated surface
Corrugated board is not one uniform bonding surface. Board grade, recycled-fiber content, liner composition, coating, printing, dust, moisture, and surface strength can vary between suppliers and lots. A surface that appears smooth may still carry loose fibers or contamination; a coated or heavily printed liner may behave differently from an uncoated liner. These conditions affect adhesive contact and the repeatability of a pressure-sensitive bond.
Avery Dennison’s corrugated paper application discussion identifies recycled-content linerboard and converting conditions as variables that can change adhesive performance. Its notes concern Avery Dennison solutions and do not provide qualification for a LubandArt grade. For a buyer trial, the practical implication is to identify the actual board sources and surface conditions rather than qualify a tape on a convenient sample that differs from production material.
Record the flute and board construction where relevant, recycled-content range if controlled by the supplier, liner treatment, print or coating in the bond area, and the condition of the board when it reaches the line. If a new board source, coating, ink, or storage condition is introduced later, treat it as a change that may require a repeat trial. Keep samples from more than one representative lot if incoming variation is part of the real process.
Check geometry and application, not only the adhesive
For a between-flap joint, map the closure geometry: flap overlap, seam width, tape placement, available bond area, carton squareness, and the gap or spring-back force when the flaps meet. The tape must reach both surfaces over the intended area. If the overlap changes with carton size or operator setup, the smallest effective bonded area may define the risk—not the average carton.
Then reproduce the application method. Note whether the tape is applied to one flap or both, whether it is transferred from a liner, the liner width and release behavior, and whether the line uses a hand process, fixture, or automatic applicator. Capture application pressure, contact time, line speed, surface temperature, and any pauses between placement and closure. A fast process can leave less time for contact and repositioning; a liner that is hard to remove can disrupt placement or create handling waste. These are process qualification questions, not properties that can be inferred from “OPP.”
One example of a double-sided polypropylene film design is tesa 61970, which tesa describes for corrugated-board carton closure and supplies with a fingerlift liner. The product page and technical product information describe that specific tesa construction. The documentation also cautions that typical values are not product specifications. This example helps explain why carrier, adhesive, and liner are specified together; it is not evidence for a different manufacturer’s tape or a substitute for testing the buyer’s carton.
Define a representative trial and pass criteria
Before running samples, have packaging engineering, operations, and quality agree what “reliable closure” means for the job. Translate the distribution and production needs into observable acceptance criteria. The criteria may cover continuous seam contact, flap retention, opening behavior, adhesive transfer, appearance, line interruption, or performance after conditioning. The buyer should set the limits and methods; do not borrow a threshold from an unrelated tape datasheet.
A controlled trial should use the production carton design, representative board lots, the intended tape model and liner, and the real application equipment or a documented simulation. Record line speed, pressure, placement location, temperature, dwell, operator steps, and environmental conditioning. Include cartons made at the start and end of a run if process drift is relevant. Inspect both immediate closure and the agreed later checkpoints after storage or conditioning.
For distribution evaluation, define the package’s actual route and expected loads with the packaging team. A transit or stacking test should represent the package, contents, pallet pattern, and handling environment, not just a strip of tape pulled by hand. If a carton opens, document whether the cause was adhesive separation, fiber tear, board failure, flap geometry, poor contact, or an application error. Different failure locations call for different corrections. Changing adhesive without determining the failure mode can add cost while leaving the underlying design problem untouched.
Also test opening if the customer or downstream operator needs controlled access. A closure that stays shut under the test but damages the board or makes opening unacceptable may fail the commercial requirement. If the package must be tamper-evident, recyclable under a particular stream, or compatible with automated case handling, make those requirements explicit and verify them with the relevant packaging stakeholders.
Approve only the exact construction that passed
The LubandArt OPP double-sided tape product page associates the product family with carton-sealing applications. The public page does not establish a named grade’s performance on recycled linerboard, automated carton closure, shipment loads, or a specific distribution test. Treat the route as a starting point for an application inquiry, not as a product approval. The existing carrier comparison guide discusses carrier families, while this article addresses carton closure qualification.
When requesting a sample or quotation, send the carton drawing, board details, flap overlap, closure location, line speed, application method, liner preference, storage conditions, and the acceptance criteria. Ask for the proposed grade’s current technical data sheet and a report or trial record that matches the actual construction and use. Confirm whether the evidence covers the exact backing, adhesive, liner, thickness, and converted format. If the construction changes, recheck the approval rather than assuming the old result transfers.
The decision is straightforward: trial double-sided OPP tape when the design can provide controlled overlap and repeatable contact, and when a representative production trial can verify the buyer’s closure requirements. Choose another closure architecture when the geometry, line handling, load path, or distribution need cannot be validated for that construction. A successful sample is evidence for the tested conditions; it is not a universal carton-sealing rating.
Frequently Asked Questions
Is double-sided OPP tape the same as common carton sealing tape?
No. Double-sided OPP has adhesive on both sides of a film carrier and may be placed between surfaces; common carton-sealing tape is typically applied across the outside of a seam. Confirm the intended closure geometry and grade.
Does a carton-sealing application on a product page prove shipping performance?
No. It is an application association, not a grade-specific package test. Request current construction data and evaluate the actual carton, line, contents and buyer-defined distribution criteria.
What should a trial include?
Use representative board lots and production cartons, reproduce overlap, placement, liner removal, pressure, line speed and conditioning, then inspect closure, openability and package-level performance against criteria set by the buyer.
Send the carton drawing, board construction, overlap, line method and speed, liner preference, storage and distribution conditions, and buyer-defined closure criteria to scope a proposed grade and representative trial.
Request a quote · [email protected] · WhatsApp +86 180 6469 2463
Need this construction for a production run?
Get a quote