
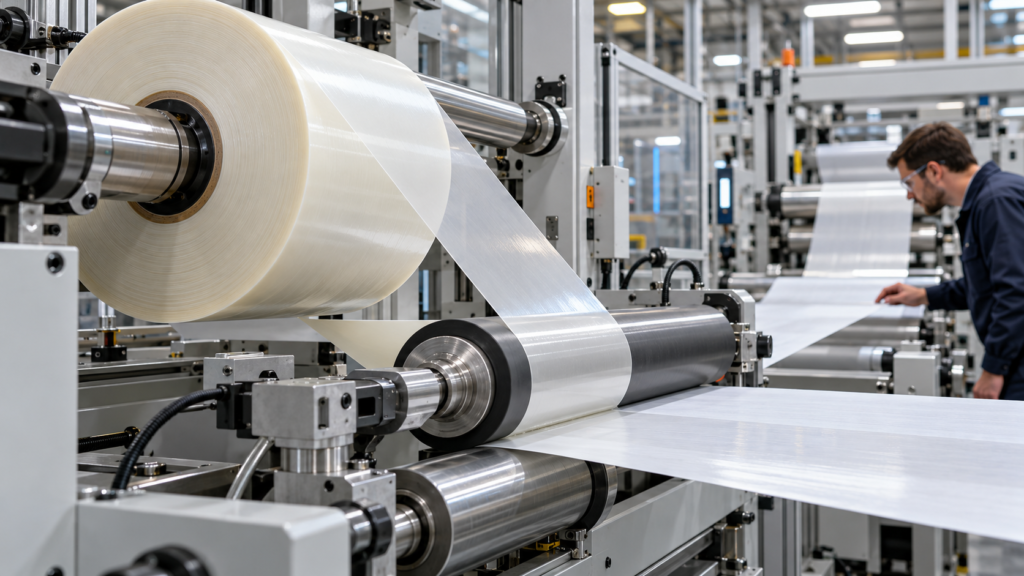
figures and test-method references in this guide are for preliminary selection only. Final performance depends on the exact construction, thickness, substrate, application and test method; request the report for the proposed grade before approval.
ASTM D3811/D3811M-21a is a low-rate unwind-force method. Its result can check an agreed limit, but it does not by itself qualify a pressure-sensitive tape roll for a high-speed converting line. For high speed tape lamination qualification, test the proposed roll under production-representative conditions.
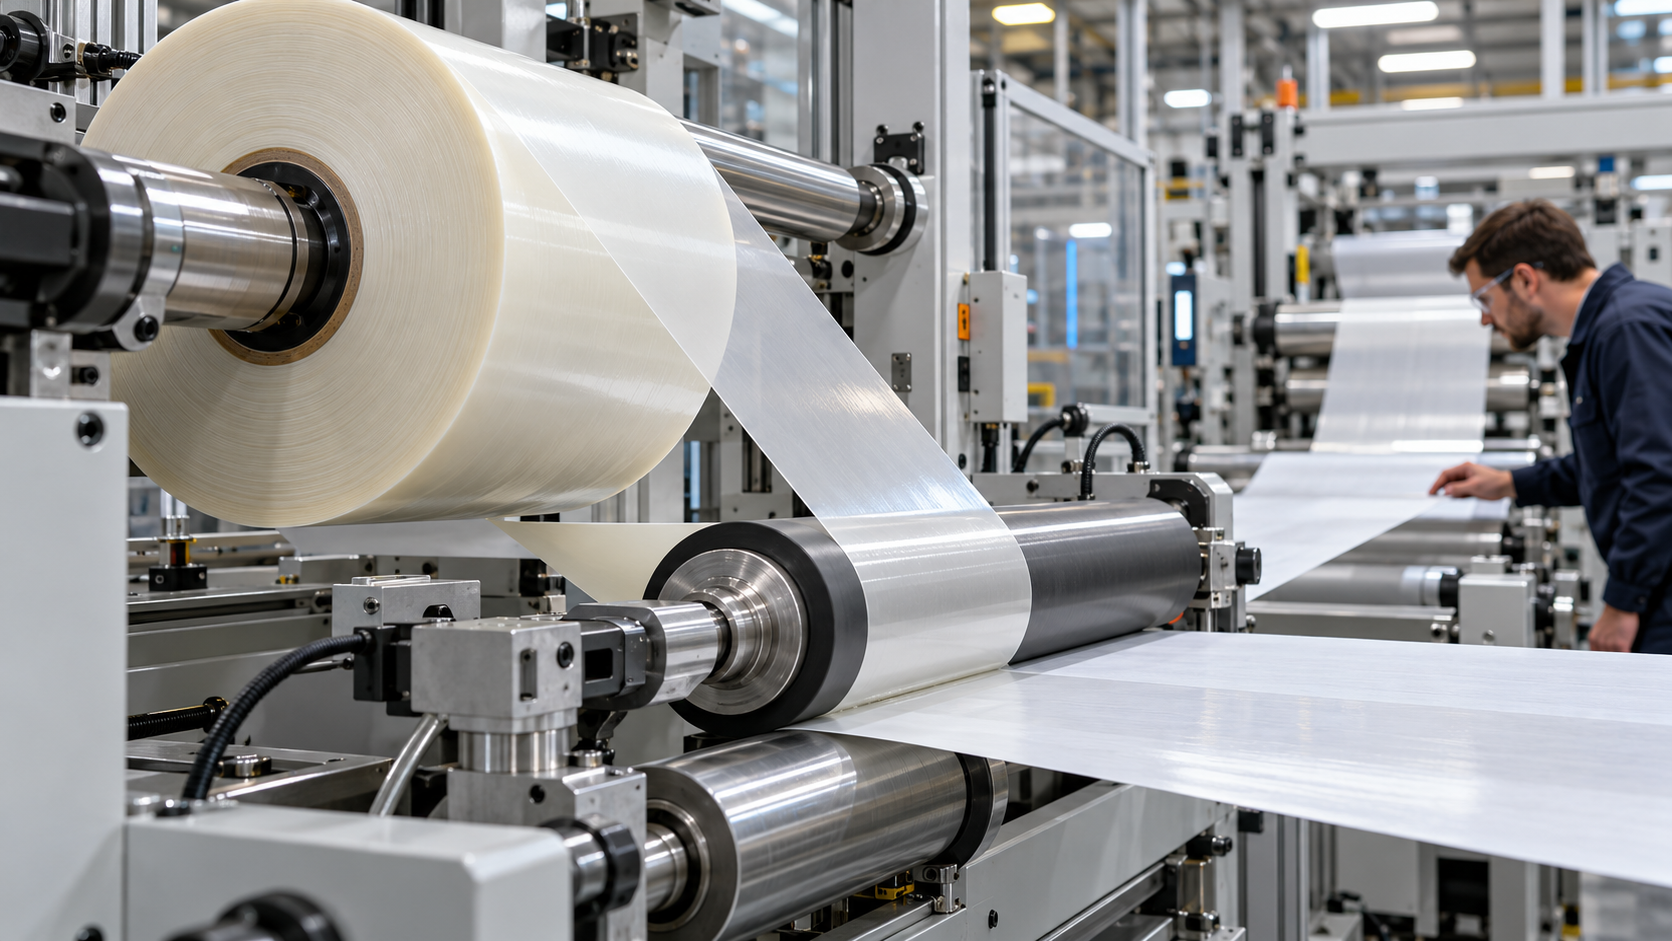
What an unwind-force result can and cannot tell you
ASTM D3811/D3811M measures the force required to unwind a roll of pressure-sensitive tape. That is useful when a buyer and supplier have agreed on a maximum, minimum or mean value and the test conditions are clear. The result can help screen incoming rolls against that requirement or compare repeat production lots tested the same way.
The important limitation is the rate. ASTM explains that its procedure simulates hand and machine unwinding at low rates. Unwind force changes with rate, and the response can invert at a rate that differs by construction and manufacturer. The method therefore does not permit comparisons of tapes unwound at high rates. A report showing a low D3811 value is not proof that a tape will run smoothly at a converter’s production speed, nor does it rank competing constructions for that line.
Use the result for the question it actually answers: “Does this roll meet our agreed low-rate unwind-force specification under this method?” Do not stretch that answer into “Will this roll run at 80 metres per minute?” unless the buyer has separately validated a correlation for the exact construction and equipment. The ASTM D3811/D3811M-21a scope and significance notes are the controlling reference for that boundary.
Keep unwind force separate from other roll and bond variables
Several values are often grouped together as “tape handling,” but they describe different events. Unwind force is the force needed to separate a roll as it turns. Release force describes separation from a liner. Web tension is the load carried by the moving tape or laminate between rollers. Nip pressure affects contact during lamination. Peel or shear strength describes a bonded specimen under a stated test. Record each measurement by method and process stage; unwind force does not substitute for liner release, web tension, nip contact or bond testing.
This matters especially when a tape has a liner. A roll may unwind acceptably but still have a liner-release level that causes the web to wander, stretch or lift at an application station. Conversely, a liner that releases cleanly does not prove the tape will stay flat through an acceleration or a long web path. The guide to PET film versus paper liners covers liner selection and converting release behavior; this article addresses the separate question of high-speed roll qualification.
Record the roll construction and the production setup together. At minimum, note tape and liner materials, width, total thickness, roll diameter, core size, winding direction, splice location, storage and conditioning, unwind direction, line speed, web path, tension setpoints, acceleration and deceleration, roller diameters, nip setting and substrate. If the line uses more than one unwind station or a dancer, record those control modes too. Without this context, a “good” result is difficult to reproduce or compare.
Why speed and tension can change the line result
A line can behave differently from a bench unwind because the web is pulled through multiple rollers and experiences acceleration, friction and alignment constraints. Excessive or uneven tension can stretch a tape or liner, shift registration, create wrinkles or pull a laminate away from its intended path. A sudden speed change may expose a control problem that a steady low-speed run does not reveal.
For its named acrylic foam products, 3M’s application guidance discusses minimizing tension and stretch, maintaining constant speed, and avoiding rapid acceleration that increases stretch. It also relates stretch to laminating roller diameter and describes pressure recommendations for those specific products. Those figures are not LubandArt specifications and should not be transferred to another adhesive system. They are useful as a reminder to include tension, speed, acceleration and roller geometry in a trial plan. See the 3M application guidelines for the exact product scope.
Nip conditions also matter. 3M’s converter guidance says roll pressure should be uniform across the web and tied to adhesive, substrate and roll conditions. Non-uniform pressure can contribute to wrinkles or steering; premature contact before the nip can trap air. These are process relationships, not universal settings. Use the converter lamination guide as a troubleshooting reference for the systems it covers, then set values on your own equipment.
Build a production-representative qualification trial
Start with the failure the line needs to prevent. Is the concern web break, telescoping, wrinkles, edge lift, liner pop-off, registration drift, adhesive transfer, poor wet-out or a finished bond that fails after conditioning? Each outcome needs its own observation or measurement. Avoid a vague pass condition such as “runs well.”
Run the candidate on the intended equipment with the actual substrate, liner-removal sequence and converting path. Keep the first comparison controlled: hold the substrate and line setup constant while changing one tape construction at a time. Include the roll diameter and lot you expect in production. If the buyer expects a range of roll diameters or ambient conditions, test the relevant endpoints rather than assuming the smallest sample roll represents every case.
The trial should cover a steady run at the target rate and the transitions that happen in real production: start-up, acceleration, deceleration, splice passage, stops and restart. Log actual speed and tension rather than only the machine setpoint. Inspect across the web for wrinkles and tracking, and along the roll for edge damage, telescoping or uneven winding. Check liner behavior and registration where the tape is laminated or die cut. If the adhesive bond is part of acceptance, allow the specified dwell and conditioning before testing it; an immediate handling check is not an adhesion qualification.
Use a repeatable sheet for every run: material and lot IDs, roll dimensions, line and roller setup, speed profile, tension readings, nip setup, room conditions, defects, downtime and sample disposition. Record the actual construction, speed profile, tension, defects, registration and any downstream bond result; set sample count and thresholds before the trial. Define the sample count and the pass/fail thresholds with the process owner before the trial. The threshold may be a maximum defect rate, registration tolerance, measured tension window or downstream bond result, but it must come from the buyer’s process requirement. Public sources do not establish a universal acceptable value for a different line.
Diagnose the failure before changing the tape
If a roll runs poorly, first separate a material issue from a setup issue. Confirm the roll was stored and conditioned as specified, the unwind brake or torque control is operating correctly, the web path is aligned, idlers rotate freely, and tension sensors are calibrated. Check whether the issue occurs at a particular roll diameter, line speed, acceleration or splice. A defect tied to a speed transition points to a different cause than a defect present throughout a constant-speed run.
Then inspect the laminate. Wrinkles can be associated with uneven tension or nip pressure; bubbles can result when the adhesive contacts the substrate before the pressure point; edge lift may involve stretch, liner behavior, contamination or bond design. These symptoms are clues, not diagnoses. Compare the line record with the known-good roll and change one variable at a time. The surface preparation and bond strength guide is relevant when the web runs cleanly but the finished bond fails on the substrate.
Do not compensate blindly by increasing nip pressure or lowering unwind tension. A change may hide one defect while creating stretch, liner separation or a new registration problem. Ask the tape supplier for the exact construction and roll-converting details, then confirm the proposed adjustment on the line.
Put the decision into the purchase specification
For a roll intended for high-speed lamination, request both the test result and the evidence needed to connect it to your process. State the ASTM D3811 edition and test condition if a low-rate unwind-force limit is required. Separately state the target production rate, roll format, liner-removal method, tension-control mode, acceleration profile, nip arrangement, substrate and acceptance checks for the actual line trial.
Ask the supplier to identify the proposed grade, adhesive system, carrier or foam, liner, thickness, width, core, roll diameter and winding direction. Request a report for the exact proposed construction when a grade-specific value is part of approval. A result from a different thickness, liner or product family should not be treated as interchangeable without evidence.
The practical decision is conditional: use ASTM D3811 for a defined low-rate unwind-force requirement, and use a controlled production trial to qualify high-speed web behavior. A configurable acrylic foam tape roll may be a candidate when the application calls for that construction, but the product family page does not establish a grade-specific line speed or unwind limit. Share the roll specification, line conditions and failure criteria when requesting a sample review.
Frequently Asked Questions
Does ASTM D3811 prove that tape will run at a specific high line speed?
No. ASTM D3811/D3811M-21a is a low-rate unwind-force procedure and says its rate does not permit comparisons of tapes unwound at high rates. Use a production-representative line trial for speed qualification.
Is unwind force the same as liner release force?
No. Unwind force measures separation as the roll turns; liner release describes separation at the liner interface. Specify and test the property that matches the failure mode.
Which conditions should a high-speed tape trial record?
Record construction, roll format and diameter, line speed profile, tension-control mode, web path, acceleration, roller and nip setup, substrate, defects and buyer acceptance criteria.
Send the proposed grade, roll dimensions, liner, target line speed, web path and acceptance criteria to request a production-representative sample trial.
Request a quote · [email protected] · WhatsApp +86 180 6469 2463
Need this construction for a production run?
Get a quote